Engineering · Workplace organisation · Packaging
65 machines, a new way of working: void fill at every workstation
I worked on the project to deploy 65 machines producing paper void fill directly at workstations. With FROMM, we started a phased rollout to free up space, improve workplace organisation and bring materials to their point of use.
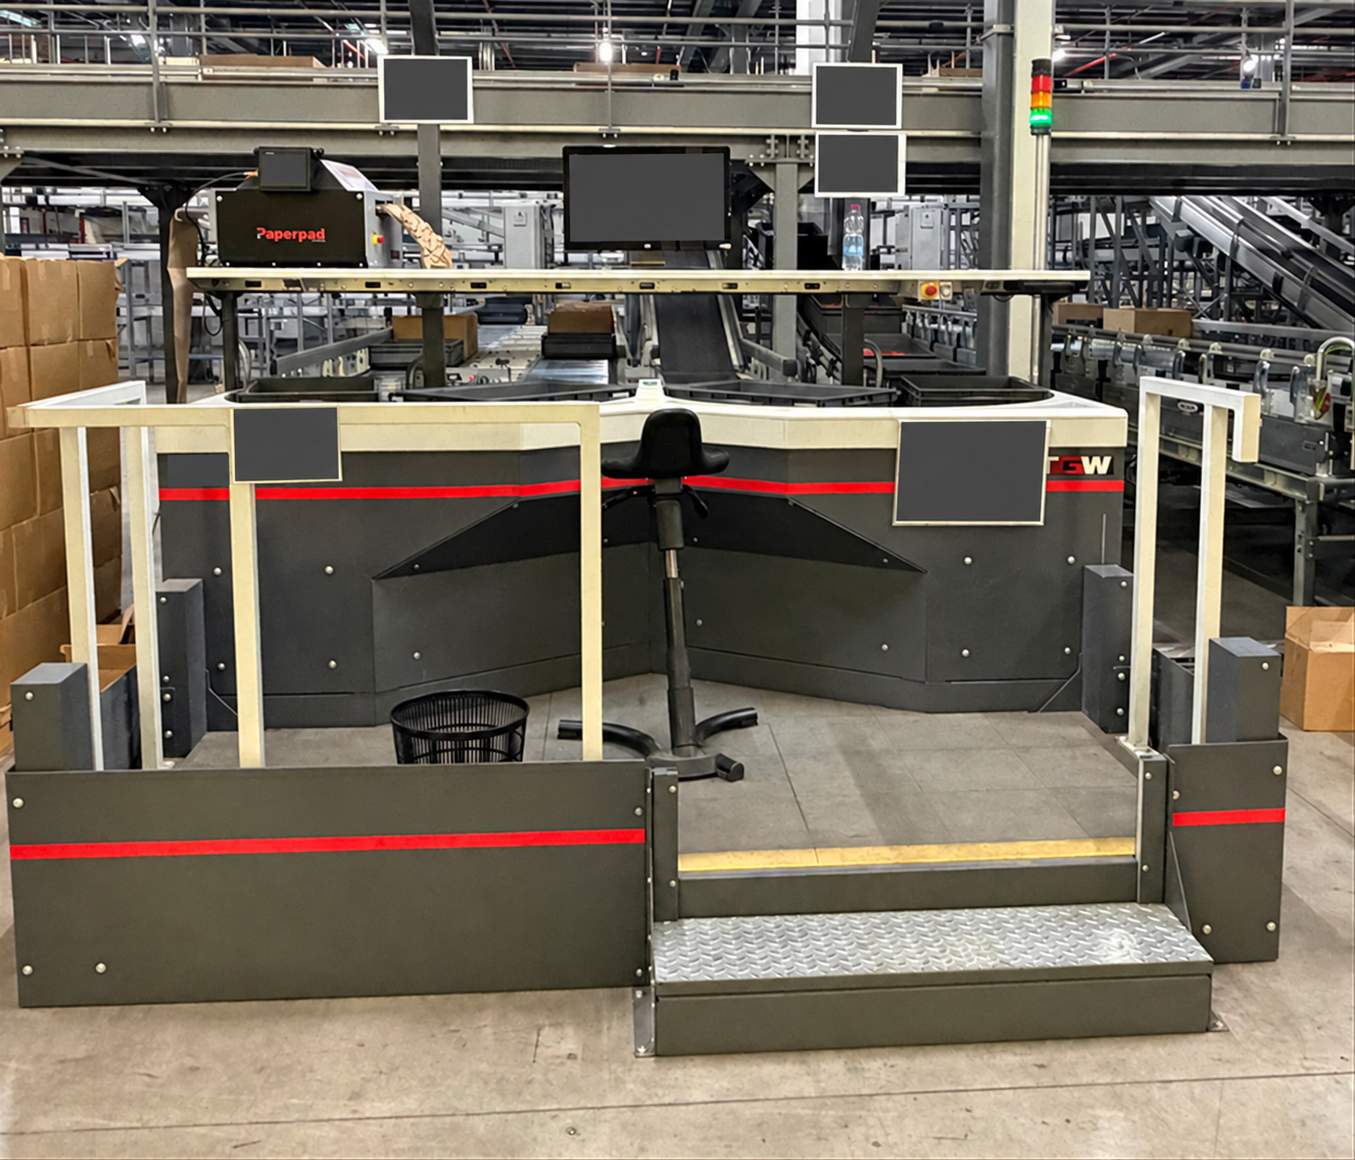
The project I am working on covers 65 machines. The first 32 PCO stations are operational; expansion to PTG and VAS stations is planned by the end of September 2026.
01 / Putting materials where they are needed
In an automated warehouse, even filling empty space in a carton can generate preparation work, material movements and clutter. Previously, paper was produced at shared points and prepared in boxes for delivery to workstations. These boxes occupied platform space and required replenishment and handling.
The project redesigns that flow: a dedicated machine produces paper at its point of use. Operators can access it during packing without accumulating boxes of pre-produced void fill in their working space.
02 / Order, cleanliness and room to work
The first observed result concerns the PCO picking stations. Removing paper boxes from the platforms after installation made the workstations tidier and gave operators more room to move and work. This practical benefit is recorded in the internal commissioning communication.
Having material at the workstation makes it easier to keep the area clean and organised. Efficiency comes from the combination of proximity, less clutter and a repeatable method. Paper-pack replenishment and routine cleaning still need to be organised; installing machines does not eliminate those tasks.
03 / Engineering: one machine per workstation
The specification established a distributed architecture with one machine per workstation. This reduces reliance on a shared void-fill production point and limits the reach of a single-unit failure, without implying downtime can be eliminated.
Integration required attention to equipment footprints, mounting supports, electrical supplies, paper loading and operator movement. Bench-mounted and trolley configurations accommodate different layouts. Placement must preserve access routes and emergency devices, with checks by plant and safety teams.
04 / A choice grounded in field trials
Three suppliers were assessed. The test plan covered paper consumption per parcel, sheet dimensions and operating conditions: paper price alone does not explain process cost or quality.
Early trials highlighted the importance of the support’s actual footprint, the paper’s ability to hold its shape, the number of operator movements and settings retention. These observations relate to configurations and prototypes assessed during selection; they are not blanket criticisms of the final solution.
The selected solution is FROMM Paperpad PC1000. The manufacturer specifies an adjustable speed of up to 40 m/min; the selected paper is 85 g/m² in 235 m packs. These are declared product specifications, not measured warehouse throughput. Supplier documentation describes the paper as 100% recycled and recyclable; this is not evidence of a measured project-level emissions reduction.
05 / FROMM: an essential partnership
Collaboration with FROMM was fundamental to translating operational needs into a solution suited to real workstations. The process combined technical discussions, field trials, configuration selection and installation support.
For me, the partnership’s value lies in discussing what works on the floor and what needs adapting, to balance product protection, ergonomics and operational continuity. My thanks to FROMM and the colleagues involved in assessment, implementation and commissioning.
06 / From the first 32 PCO stations to wider deployment
In the first phase, we completed installation at 32 PCO stations, now operating with dedicated machines. The project covers 65 machines in total: expansion with trolley-mounted systems to line-picking stations (PTG) and value-added and quality-control activities (VAS) is planned by the end of September 2026.
A phased deployment supports change on the warehouse floor: checking equipment placement, organising consumables and establishing operating practices before expanding to other layouts.
07 / Sustaining and measuring the benefits
Tidier platforms and more working space are commissioning observations. Quantifying steady-state efficiency requires comparing paper consumption per parcel, replenishment times, interruptions and packaging quality across comparable periods and order types.
Cost simulations supported the assessment but are not presented as realised savings. The objective is to improve the whole flow without moving problems downstream: unsuitable paper can increase parcel height or create rework.
Efficiency takes shape at the workstation
A dedicated machine, a clearer platform and materials in the right place: simple ideas that require analysis and integration to work at scale. The FROMM project brings that principle into daily operations, focusing on people and process continuity.
Confidentiality
Prices, costs and confidential information are not published.